Application selection example

Battery Tab Weld Height Inspection

Application route for battery tab, weld and height checks where 2D contrast alone may not prove geometry. This in-house example proposes 3 acceptance checks and 4 RFQ inputs. It does not report completed customer testing or achieved performance.

Battery tab and weld inspectionHeight, profile, presence and traceability route3 measurable checks before quote
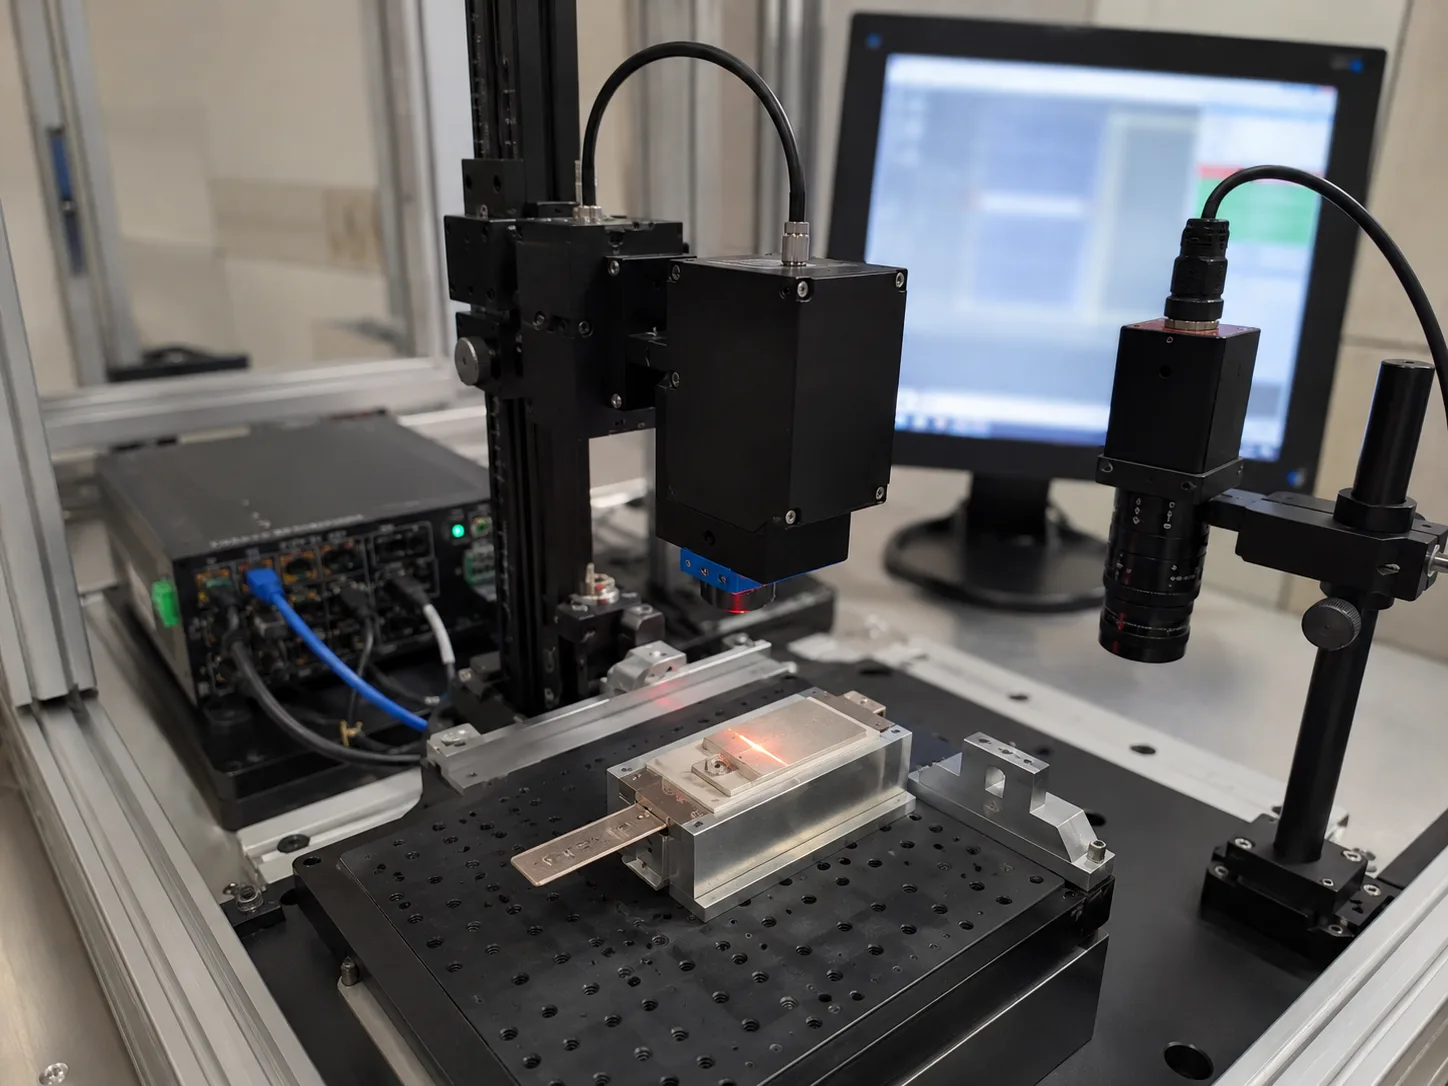
Illustrative application visual: Battery tab weld height inspection station with industrial vision hardware
In-house worked example

Height, profile, presence and traceability route

Best used when 2D contrast cannot prove weld geometry and a measurable height or profile route is required.

Battery tab and weld inspection Illustrative planning assumption: 3-6 week profile test and station timing review
Hardware stack

Component candidates to review before a project-specific quote.

3D vision or laser profiler2D alignment cameraControlled lightingData handoff to line system
Inspection challenge

What makes this scenario difficult?

Battery tab weld inspection needs geometry confidence, stable position reference and traceability under high station throughput.

Recommended route

Which component route should be reviewed first?

Evaluate 3D vision or laser profiling for height and profile checks, with 2D cameras supporting alignment, presence and traceability tasks.

Acceptance target

How should the result be validated?

Height or profile repeatability target defined before quote

Case decision frame

Use this route only after the production constraint is measurable.

Worked examples explain the problem, assumptions, component candidates and evidence a project needs. Use these four fields to prepare a test plan for your own application.

Problem

Battery tab weld inspection needs geometry confidence, stable position reference and traceability under high station throughput.

Production constraints

Height or profile repeatability target defined before quote Reflective weld samples tested for missing profile data

Hardware stack

3D vision or laser profiler + 2D alignment camera + Controlled lighting + Data handoff to line system

Next evidence to send

Weld sample photos or video, Height tolerance note, Cycle-time constraint

Inspection workflow

Steps to validate this application route before hardware selection.

The right product family depends on measurable samples, line conditions and acceptance criteria. Use this workflow to move from application idea to testable project evidence.

  1. Define weld height or profile tolerance Define the measurable weld height, profile or presence tolerance before choosing 2D or 3D.
  2. Check reflectivity and motion condition Check whether reflectivity, movement or station vibration creates missing profile data.
  3. Test 3D field width and resolution Match 3D field width, height resolution and cycle time to the weld area.
  4. Confirm pass/fail data handoff Define pass/fail data, image/profile storage and station handoff before quotation.
Proposed acceptance targets

Checks to agree and validate before a project-specific quote.

  • Height or profile repeatability target defined before quote
  • Reflective weld samples tested for missing profile data
  • Station timing compared with takt-time requirement
Sample evidence

Sample information to provide for your own application.

Weld sample photos or videoHeight tolerance noteCycle-time constraintOutput protocol note

Example boundary

This is a selection exercise, not an anonymized customer project.

These routes show how a selection decision is reached and what is checked before acceptance. Numeric values and planning windows are example targets, not achieved results or promised lead times. These are not audited performance figures, not a customer reference list, and not a claim that any particular buyer ran this route.

Not applicable. These routes are illustrative — worked examples of how a selection decision is reached, written in house. No engagement, buyer or site sits behind any of them, so there is no party whose permission could be sought. This is not a record of consent obtained; it is a record that consent has no subject here.

Application visuals are illustrative and are not offered as photographs of a customer installation. Numeric checks and planning windows are example targets, not measured outcomes or promised lead times.

Related product families

Start the hardware review with these component routes.

View all products

Related solution and selection pages

Where this case leads next.

View resources

Application RFQ

Need a route for battery tab weld height inspection?

Send sample images, line speed, tolerance and the current failure mode. We will map the application to camera, lighting, lens, reader, 3D or smart camera routes.

Request engineering RFQ
Proposed validation plan

Example checks to agree before hardware is recommended

Battery Tab Weld Height Inspection — proposed checks, not achieved results. Illustrative planning assumption: 3-6 week profile test and station timing review
# Proposed acceptance check to validate
1 Height or profile repeatability target defined before quote
2 Reflective weld samples tested for missing profile data
3 Station timing compared with takt-time requirement

Application FAQ

Clarify the application route before selecting hardware.

Ask engineering
Is battery tab weld height inspection a customer delivery record?

No. This is an in-house application selection example for battery tab and weld inspection. No customer engagement, buyer or site sits behind it. The component route, sample requirements and numeric acceptance targets are proposals to validate, not achieved results.

What should I send for a battery tab weld height inspection RFQ?

Send weld sample photos or video, height tolerance note, cycle-time constraint, output protocol note. Include good and bad samples whenever possible so engineering can test the route before recommending hardware.

Which product families are usually involved?

3D Vision Cameras, Industrial 2D Cameras, Machine Vision Lighting are the first product families to review, but the final route depends on sample images, speed, tolerance and installation space.

What information should I send before requesting a machine vision quote?

Send part photos or drawings, target defect or measurement goal, field of view, working distance, line speed, accuracy target, lighting limits and any current camera, lens, light, barcode reader or competitor model.

Do I need a 2D or 3D machine vision system?

Use 2D when contrast, edges, labels or position are enough to judge the part. Use 3D when height, profile, gap, volume, weld shape or surface geometry decides pass or fail.

How should I choose machine vision lighting?

Start from the defect and material surface instead of the camera model. Backlight helps edge measurement, coaxial and dome lighting help reflective surfaces, and bar or ring lighting often works for general presence and defect checks.

Continue troubleshooting

Contact

Direct RFQ contact

Talk to engineering about the inspection problem.

Send sample images, competitor model, FOV, working distance and line speed before model selection.

Target: selection brief within 24h
Send sample images